How to Choose the Right PLC HMI Control Panel?
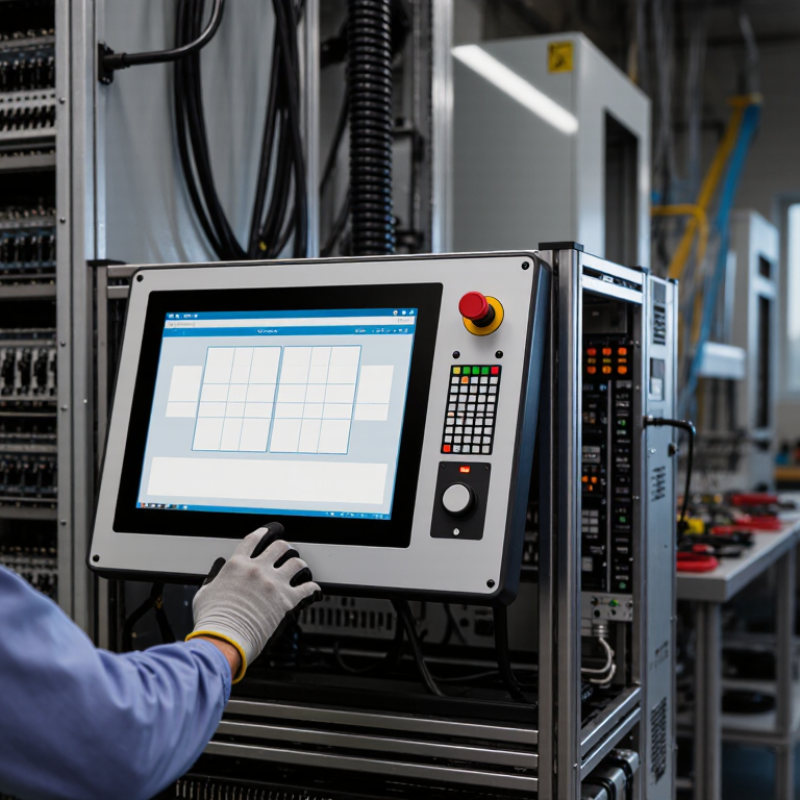
Choosing the right Plc Hmi Control Panel starts with the machine, not the screen. List the tasks operators must perform, the information they need at a glance, and the conditions around the installation. A packaging line may need clear alarm messages and quick recipe changes. A dusty workshop may require a sealed front panel and a display that remains readable under bright lights. Small details matter. Screen size, mounting depth, power supply, and operating temperature should match the control cabinet and work area.
Next, check compatibility with the PLC, network, and existing software. Confirm supported communication protocols, available ports, and whether the panel can display the tags and alarms your project requires. A familiar-looking interface is not enough. Operators wearing gloves may need larger touch targets, while maintenance staff may depend on clear diagnostic screens. Also consider cybersecurity updates, data backup, and access controls. These are practical reliability questions, not optional extras.
The lowest purchase price can hide costs in configuration, training, or future replacement. Compare the total installation effort, warranty terms, spare-part availability, and supplier support. Ask for a demonstration using realistic screens or a representative project, rather than relying only on a brochure. It may still be hard to predict every future need. That is worth admitting. A sensible choice balances present tasks with reasonable room to grow, without paying for features the machine will never use. When requirements remain uncertain, document the assumptions and verify them with the controls team before ordering.
Define PLC I/O, Logic, and Network Requirements Using IEC 61131-2
Choosing a PLC HMI control panel starts with a clear I/O list. Count each sensor, valve, motor command, and spare point. For every signal, record voltage, current, isolation, and response time. IEC 61131-2:2017 specifies functional and electromagnetic compatibility requirements and tests for PLC equipment and peripherals. It does not select your network protocol or design your control logic. Check input type and thresholds, especially for 24 V DC signals. Confirm output ratings against real loads, including startup current.
Define logic requirements in practical terms: sequence steps, interlocks, alarm states, and what happens after power loss. Record the slowest acceptable response, not just the normal scan time. Then map network traffic between the PLC, HMI, remote I/O, and supervisory systems. Set protocol, update rate, cable route, and recovery behavior. Deloitte’s 2025 Smart Manufacturing Survey reported that 92% of surveyed manufacturing executives saw smart manufacturing as a competitiveness driver over the next three years. That ambition still needs a modest, reliable network plan.
Tips: Test a real device at the end of the longest cable run. Document the measured I/O values and recovery time. It is easy to overlook noise or startup delays; I have seen a tidy design feel less tidy on the factory floor. Recheck the panel against the applicable IEC 61131-2 edition and the equipment documentation.
How to Choose the Right PLC HMI Control Panel?
Define PLC I/O, logic, and network requirements using IEC 61131-2
For the illustrated 24 V DC input types, signals at or below 5 V are in the OFF region; the guaranteed ON region begins at 15 V for Type 1 and 11 V for Type 3. Voltages between the OFF and ON thresholds are not guaranteed logic states. Confirm thresholds against the selected I/O module and applicable IEC 61131-2 edition. Separately document I/O counts, logic behavior, HMI update needs, and network protocol and timing.
Set HMI Display and Alarm Requirements with ISA-101 Usability Principles
When specifying a PLC HMI, define what operators must notice and do before choosing screen size or graphics. ISA-101 offers guidance for usable process displays, not a fixed visual template. Build a clear hierarchy: an overview for plant status, followed by focused screens for equipment and details. Keep navigation, labels, units, and symbol meanings consistent. Use restrained backgrounds and reserve strong colors for conditions that need attention. A flashing red pump icon may attract the eye, but if ordinary states also use red, the signal loses meaning. Test the layout at the actual viewing distance, including glare and glove use. Small text can look fine on a desk. Not always.
Set alarm requirements around operator action. Each alarm should identify the affected asset, the abnormal condition, and a practical response. For example, “Tank 2 level high—check inlet valve” is more useful than “Level alarm.” Define priorities by consequence and urgency, then verify that audible and visual cues match those priorities. Review alarm frequency during realistic operating scenarios; crowded banners can hide the event that matters. Keep acknowledgment distinct from resolution. Test it live. Operators should try real tasks on the screens, not just review mockups. Their feedback may expose awkward navigation or missing context, and not every first design will be right.
Select IP54, IP65, or IP66 Protection Based on IEC 60529 Conditions
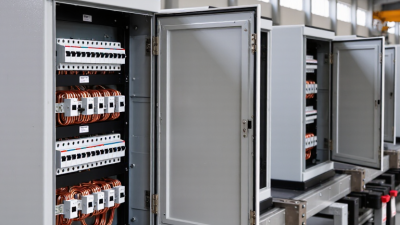
Choosing a PLC HMI panel starts with the dust and water it will actually face, not the highest rating available. IEC 60529 defines IP54 as dust-protected, allowing limited ingress, and protected against splashing water. IP65 is dust-tight and tested against water jets; IP66 is dust-tight and tested against stronger jets. These ratings describe enclosure tests, not every detail of a finished installation.
Tips: IP54 may suit an indoor cabinet exposed to dust and occasional splashes. Consider IP65 where water jets are likely, and IP66 where stronger jets are expected. Check the ratings of cable glands and connectors too. Check the seals.
IEC 60529’s test data makes the difference concrete: the IPX5 water-jet test uses about 12.5 litres per minute, while IPX6 uses about 100 litres per minute. Neither rating alone guarantees resistance to immersion, chemicals, corrosion, or cleaning conditions beyond the specified test. A well-rated door can still leak through a poorly fitted gland. Inspect seams after installation; workmanship matters. Choosing IP66 “just in case” may add cost without solving the actual exposure.
Verify Panel Wiring and Electrical Safety Against IEC 60204-1
How to Choose the Right PLC HMI Control Panel?
Verify Panel Wiring and Electrical Safety Against IEC 60204-1
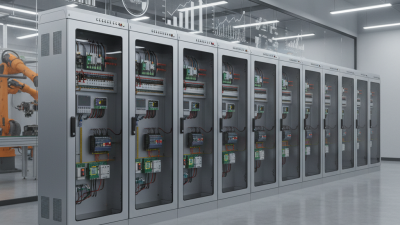
A suitable PLC HMI panel must fit the machine’s electrical design, not just its screen size. IEC 60204-1 addresses electrical equipment of machinery, including protective bonding, overcurrent protection, and disconnecting means. Check that the panel’s supply voltage, fault-current rating, and environmental rating match the installation. A mismatch can turn a tidy cabinet into a service problem. Small details matter.
Inspect the wiring plan before choosing the panel. Confirm that protective conductors connect securely to the enclosure and that terminals are clearly identified. Separate power wiring from sensitive control and communication cables where practical. Check that cable entries preserve the enclosure’s rated protection. Leave enough room to bend conductors without pressing them against sharp edges. A drawing can look perfect, yet miss a crowded terminal row; review the actual layout, too. Verify requirements against the applicable edition of the standard and have qualified personnel assess the design.
Tips: Ask for wiring diagrams, terminal schedules, and protective-device details. During inspection, look for loose strands, missing labels, and blocked ventilation. Record any mismatch and resolve it before energizing the machinery. I would recheck access for maintenance as well; it is easy to overlook when space is tight.
Compare Lifecycle Support, Spare Parts, and Total Cost of Ownership
Choosing a PLC HMI control panel means looking beyond its purchase price. Check how long the manufacturer supports the operating system, firmware, and communication protocols. Ask whether replacement screens, power supplies, and communication modules will remain available, and request realistic lead times. A low-cost panel can become expensive if a failed touchscreen sits in a warehouse for weeks.
Total cost of ownership includes hardware, engineering, training, spare parts, and production losses during faults or upgrades. The 2024 True Cost of Downtime report estimated that downtime can cost large companies around 11% of annual revenue. That figure will not predict one plant’s losses, but it shows why response time matters. Compare service coverage and repair procedures alongside purchase quotes. Also check whether technicians can restore a project from a readable backup. Small detail. It is often missed.
Tips: Price a five-year support plan, not just the panel. Keep a compatible spare for critical lines, and test backup restoration before commissioning. Record expected firmware support and parts lead times in the purchase evaluation. Then compare those costs with the value of production time at risk.
 Intelligent Manufacturing / Industry 4.0
 Motor Control Center MCC
 Data Center
 Environmental Industry
 Industrial Machinery
 New Energy
 Pharmaceutical Manufacturing
 Petroleum & Chemical
 Marine & Offshore & Ship
 Food processing / agricultural production